


Qingdao Ruiyuan Cell Technology Biotechnology Development Co., Ltd. is a biotechnology company professionally committed to providing personalized cell storage solutions, large-scale cell culture and preparation, technology research and development, and clinical transformation. Its business covers the industrial chain of stem cells, immune cell storage, cell preparation, cell detection, and clinical scientific research transformation, as well as health management featuring tumor ultra-early screening and immune function detection and evaluation, and the large health field such as cell anti-aging. The company focuses on technological and management innovation and has been successfully recognized as a "National High-tech Enterprise," Qingdao "Specialized, Refined, Distinctive, and Innovative" SME, Qingdao New R&D Institution, Qingdao Eagle Enterprise, Qingdao Innovative SME, Technology-based SME, and Qingdao West Coast New Area Key Laboratory of Stem Cell and Regenerative Medicine, and has been approved to establish the Qingdao Autoimmune Disease Research Expert Workstation.
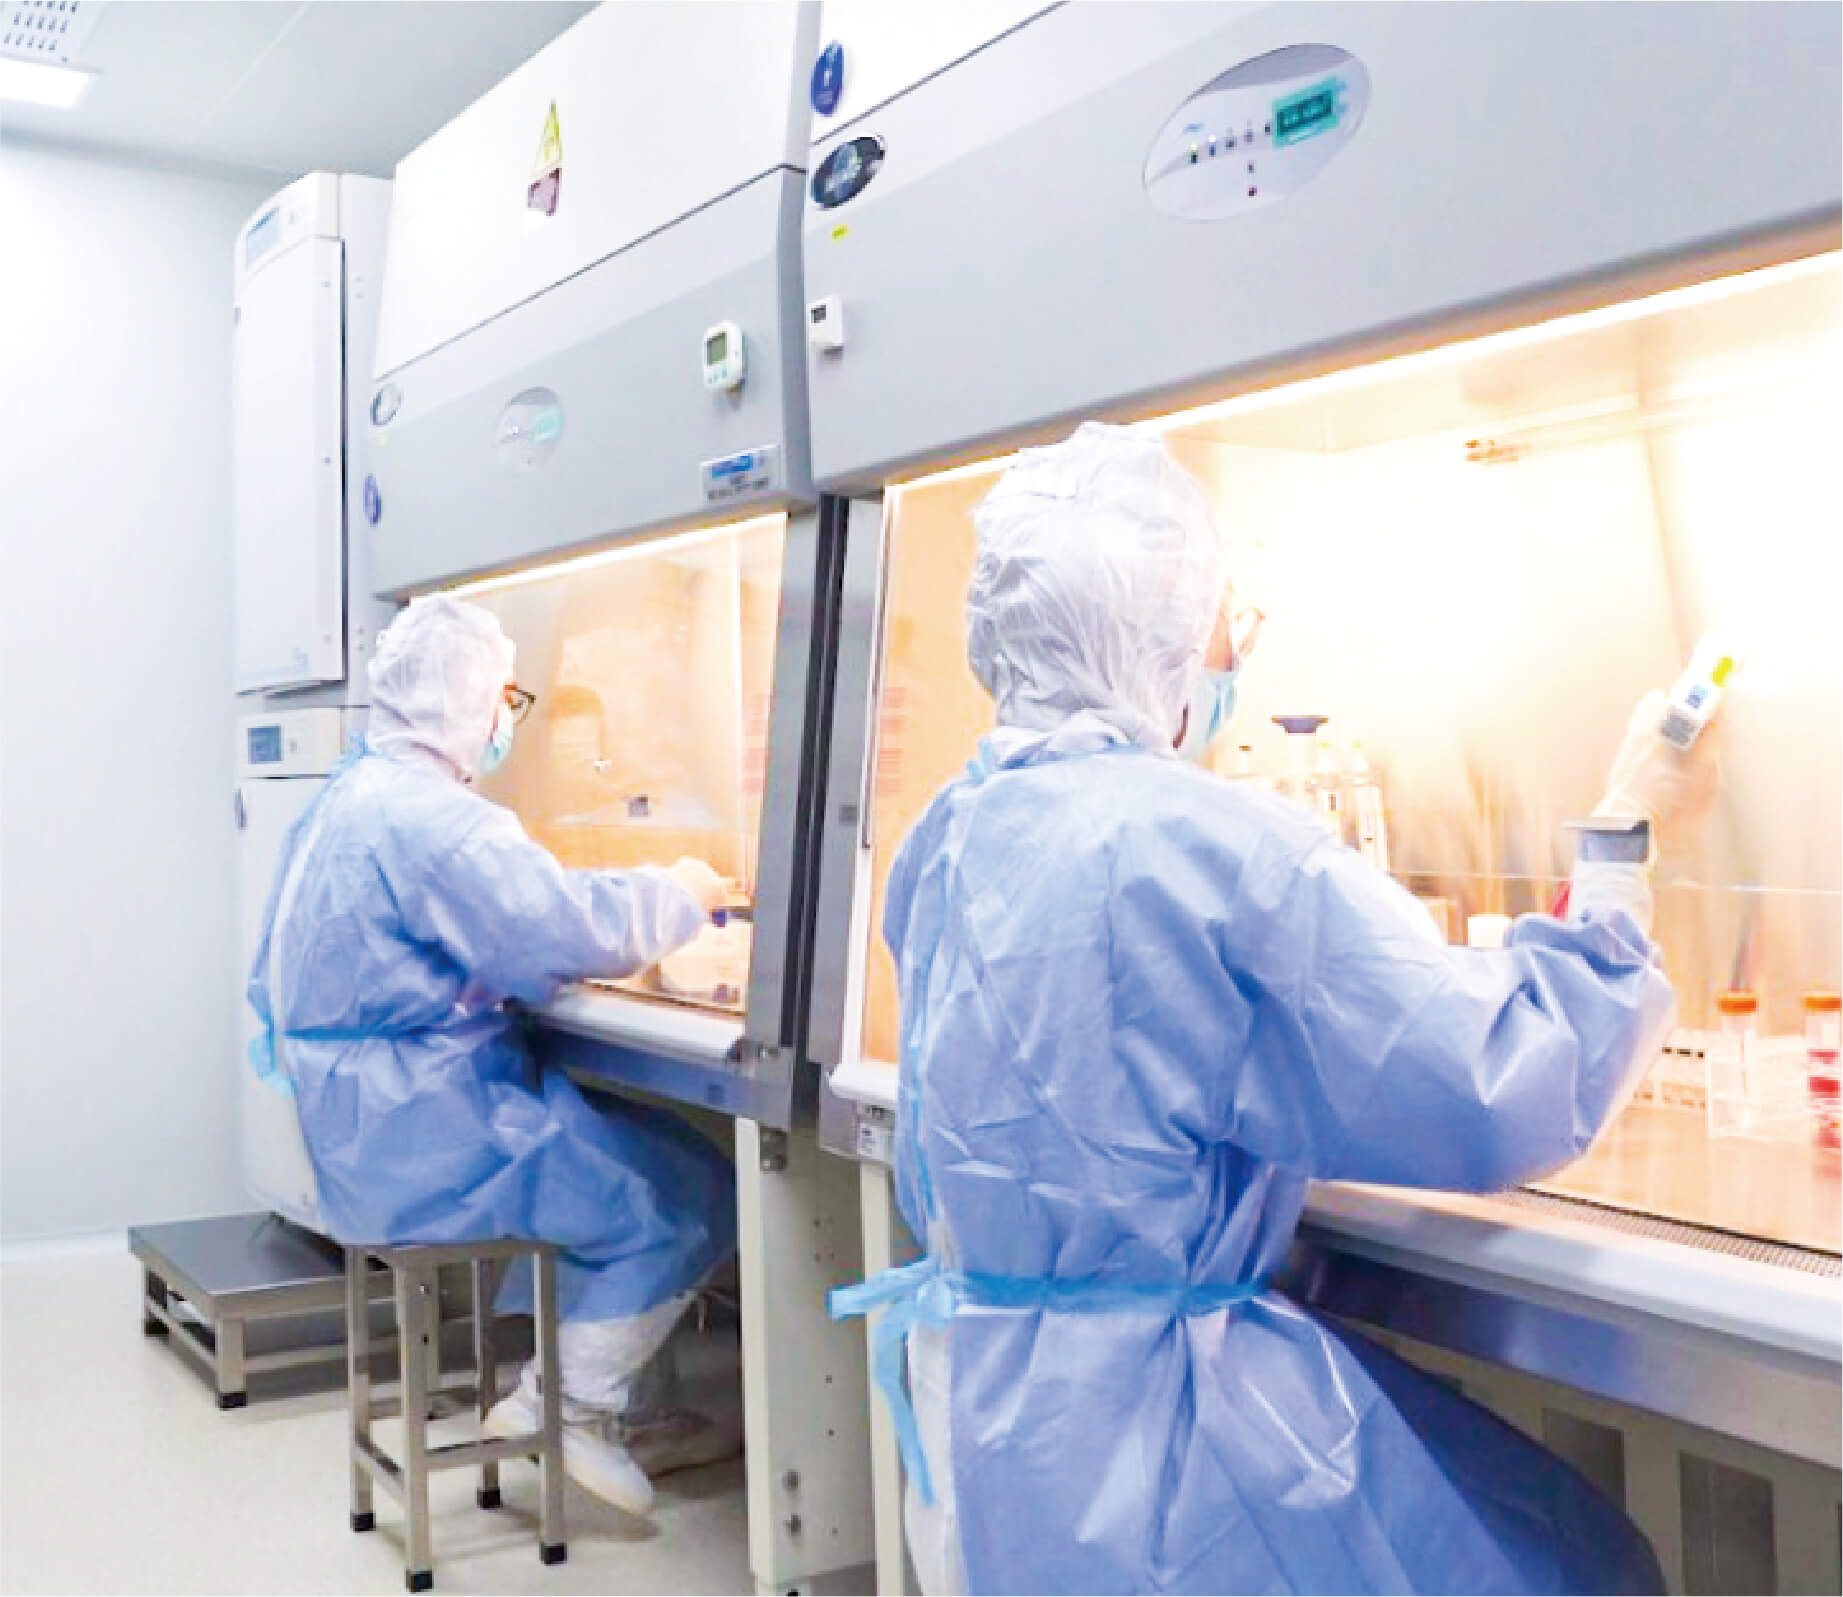
The Ruiyuan Cell Technology Laboratory is strictly designed and constructed in accordance with the Chinese Pharmacopoeia and the US AABB standards, adopting the "one-way flow" design concept. It has more than 1,500 square meters of "B+A" grade clean laboratories that meet the EU GMP production management standards, equipped with internationally advanced NuAire A2 biosafety cabinets, bioMérieux dual-temperature microbial detectors, and BD flow cytometers and other imported instruments and equipment. It has strict SOP operating procedures and a quality control system, effectively ensuring cell activity and preparation quality, and realizing standardized and intelligent management of cell resources. The cell storage bank has introduced the region's first 5G fully automated deep-low-temperature honeycomb biological sample storage system, which can realize automated operation management and efficient retrieval and information traceability of the entire process from programmed cooling, transfer, and access, significantly improving the quality, efficiency, and safety of cell storage.